Orapi Maintenance combines technical expertise and sustainable growth to shape the future of industrial maintenance
For more than five decades, Orapi Maintenance has helped UK manufacturers to solve challenges and keep production moving. A wholly owned subsidiary of the wider Paredes Group, the company’s deep technical expertise has translated into faster fixes, fewer failures, and greater uptime for the world’s leading manufacturers. From adhesives and lubricants to cleaners and corrosion protection, every product is backed by the same high-quality standards, providing consistent performance, dependable results, and peace of mind when it matters most. Today, that expertise supports the manufacturing ecosystem in more than 40 countries worldwide.
“Orapi Maintenance UK is an industrial chemical manufacturer formulating high-tech consumable solutions for the maintenance of equipment, machinery, facilities, and industrial processes,” begins David East, Divisional Director at Orapi Maintenance. “We combine product innovation with practical application knowledge, helping customers to choose the right chemical solution and apply it with confidence. Our strapline is that we provide solutions backed by technical know-how, not branding.
“We’re based in our brand-new 58,000 square foot manufacturing site in Wednesbury in the West Midlands. We moved here in late 2025 and are proud to be members of the Black Country. We currently have 49 employees split across operations and commercial. We turn over £8+ million, solving complex maintenance challenges with solutions trusted by industrial facilities across the world.”
With seven R&D laboratories and a growing portfolio of proven solutions shaped by technical expertise, Orapi Maintenance has earned the trust of some of the world’s leading manufacturers, whose teams rely on its products and recommendations every day. Championing a consultative sales approach, the company offers a comprehensive portfolio of products designed to support a wide range of industrial and manufacturing requirements. Orapi Maintenance’s offering includes clean room products, dust management solutions, industrial cleaners, solvents and detergents, as well as tracing and marking solutions and surface protection products. The portfolio also covers an MRO range – greases, oils and dry lubricants, release agents, adhesives, and sealants – along with a wide range of water treatment additives.
“We’ve got longstanding relationships with our customers that go back 20+ years,” David elaborates, reflecting on the company’s key differentiators. “We’ve broadened our approach to customer service, as many of our customers didn’t realize that we provided products in other catalogues; for example, our competitors in the dust management sector don’t offer the full product range that we do in other categories. The products that we manufacture are underpinned by consistent high quality and first-class customer service.”
These commitments are also reflected in the company’s ongoing investment in its operations. As David previously stated, a significant milestone came in 2025 when the business moved to new headquarters, providing an opportunity not only to secure its future but also to rethink and modernize the way it manufactures and engages with customers.
“Our previous landlord wanted to redevelop the site, so we were somewhat pushed into the move, but it’s been absolutely superb for the business,” Mark Pearson, Manufacturing Director, explains. “We’re an old-established company that operated with old methodology, so this move has allowed us to redevelop and redesign our manufacturing processes and bring the company into the 21st century. Customers can now also come to our facility and see, touch, and feel our manufacturing processes, which we’re now able to use as an additional selling tool for the business.
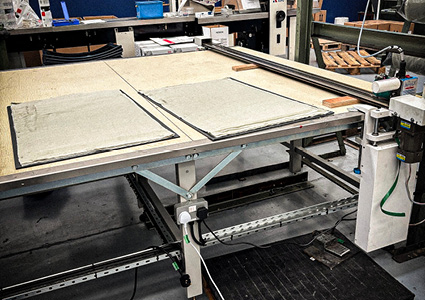
“In this facility, we’ve redesigned the way that we operate to increase our capacity through our production lines, making them cleaner, safer, and quicker at the start of the process,” Mark continues. “At the end of the line, we’ve changed the way that we pack with ergonomic desks for all our packers. We’ve also implemented this methodology into another production line: the TAKmat. We bought an air fed table which helps us to move products more easily along the production line, whilst also providing health and safety benefits.”
With the foundations of a more modern and efficient operation now firmly in place, the company is turning its attention to the next phase of its development, with a clear focus on building further momentum for the future.
“We’re currently developing an eco-friendly, water-based resin product that can carry out the same function as oil-based resin, but can be disposed of through natural waste streams,” Mark reveals. “Certain elements of that technology have already been proven, but the project is still in its embryonic stage, and we need to invest in the machinery to carry out this function.
“We are holding our first defense event in our new facility in September. The event will be themed around the West Midlands Combined Authority (WMCA) and how to get into the defense sector, and we have big names like Babcock, Safran, and Collins Aerospace on site. It will be a very topical and extremely well-funded,” David adds. “Plus, this quarter, we’re also launching our new distributor partnership program. We’re aiming to work with some of our smaller distributors to improve their business, and have put together a wide range of development and support tools to ensure that this program develops with traction, whether that be by training them or their customers or bringing them to the lab, to name a few.”
With a modern manufacturing base, decades of technical expertise, and a clear commitment to innovation, Orapi Maintenance is well-positioned for its next chapter. From developing more sustainable solutions to strengthening its distributor network and exploring new opportunities across emerging sectors, the company is continuing to evolve while staying true to the quality, service, and practical know-how that have underpinned its success for more than 50 years.
“We’ve got a six-year plan from 2026 to double our turnover; I made a promise to our CEO that we’d grow to be a €20 million business. We’re currently the biggest subsidiary across the Group, so we want to be high growth, innovation-led, and able to deliver sustainable, profitable value. We want to diversify our markets and use advanced technology to have world-class operational excellence,” David affirms.
“In particular, in the defense market, we’re looking to partner with some of our pre-existing distributors. We’ve got dedicated support on defense and we’re seeing major growth opportunities there. Our process can be easily adapted to accommodate any certification needed for any given marketplace. That’s a big focus area for us right now.”