
Autonomous robots are only as smart as the factory around them
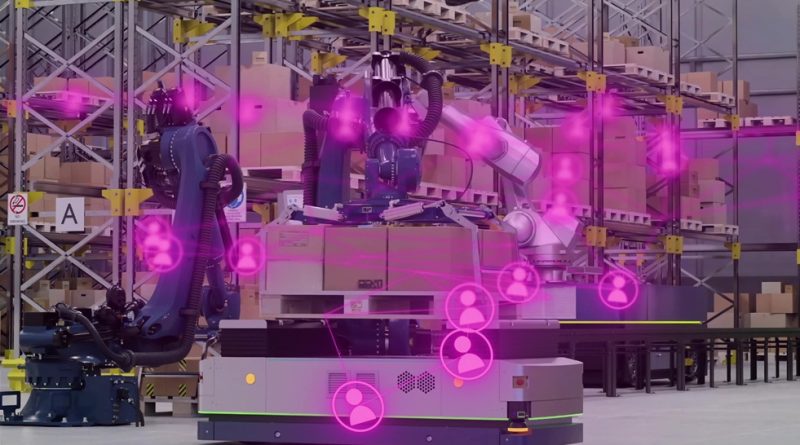
At Rockwell Automation’s Twinsburg manufacturing facility, autonomous mobile robots were moving materials around the factory, but people were still telling them when to move. The transport had been automated without changing the process that controlled it, leaving much of the potential improvement in production efficiency unrealized.
For Ara Surenian, Senior Product Manager at Rockwell Automation, the experience illustrates a fundamental limitation of factory automation. Replacing manual tasks with autonomous equipment can deliver immediate savings, but the bigger opportunity comes when that equipment responds directly to production demand, removing delays and unnecessary activity from the wider operation.
Rockwell’s FactoryTalk Orchestration was developed to bridge that gap. Its deployment at Twinsburg demonstrates how connecting material movement to manufacturing execution can deliver improvements far beyond those achieved by introducing autonomous robots alone.
“Often the biggest deterrent to further adoption of autonomous mobile robots is the integration,” Surenian says. “How do you bring in this new technology and have it implemented within a company’s current IT and OT infrastructure?”
The problem between production systems
Production schedules determine what should be manufactured, but the systems responsible for supplying the materials often operate independently. Even in highly automated factories, employees may still have to initiate deliveries manually, with little connection to what is happening on the production line. Components can arrive long before they are needed, occupying valuable floor space, while unexpected shortages leave operators scrambling to keep production moving.
Having previously managed production operations, Surenian understands how easily material handling can undermine the efficiency of an otherwise automated factory. The consequences extend beyond the immediate interruption, affecting production costs and the ability to meet delivery commitments.
“Somebody goes to the inventory location, picks out the stuff needed, puts it on a cart, brings it to the production line, often stages it in advance, and then as production is executing, they’re pulling the material they need, and invariably something is missing,” he says. “Or there’s a change in priority, so now the material needs to move back.”
FactoryTalk Orchestration connects material movement with production requirements through configurable workflows. Its low-code, no-code environment allows manufacturers to integrate AMRs with manufacturing execution systems (MES), warehouse applications, PLCs and other equipment. An AMR approaching a dock door can trigger a PLC to open it, while another workflow coordinates transferring a pallet onto a conveyor.
The important change is not simply that the robot completes its journey unaided. Its movements can be triggered by actual production activity rather than by an operator remembering to request a delivery.
“When you have work that’s being executed, and the material for that work is done in sync with the actual production, you’re able to reduce inventory,” Surenian explains. “You can eliminate a lot of the staging for WIP. All the back and forth and change starts going away because now everything is synced up to actual demand.”
Twinsburg demonstrates the difference
Rockwell introduced autonomous production logistics at Twinsburg in stages rather than redesigning the entire facility at once. The first phase deployed three AMRs to replace movements previously performed by employees pushing carts. Pickup points, racking and material transfer processes needed adjustment, but the robots successfully took over repetitive transport work and allowed employees to undertake other tasks.
Surenian reports approximately $165,000 in savings from that initial deployment. Yet little changed in the underlying production process because operators still decided when the robots should deliver or remove materials.
“The material triggers were human-driven. It was an operator saying, ‘I need material now, and I’m done. Material go back,’ because it was still a human-driven process,” he explains. “We didn’t really change the WIP. We didn’t change throughput. We just took what was once done by a human being, and now an AMR is doing it.”
The second phase connected FactoryTalk Orchestration with the facility’s MES. Material movement could now be initiated by digital signals reflecting what the production line was doing, reducing the need to stage inventory in anticipation of work.
Surenian reports a 70 percent improvement in space utilization, a 50 percent reduction in work-in-process inventory and a 20 percent efficiency improvement. Floor space previously occupied by materials became available for productive activities, while deliveries were more closely synchronized with demand. “We moved from a close enough in time system to a true just in time system because now the demand of production is pulling the material,” he says.
The third phase extends the approach to two MES systems, maintenance applications, automated storage and retrieval equipment and an expanded fleet of approximately 18 AMRs. The team also uses Emulate3D to simulate and test workflows. Where the initial investment automated transport, orchestration subsequently improved the wider operation.
Integration is the hard part
Brownfield manufacturing facilities rarely have standardized technology environments. Older control systems coexist with enterprise applications, warehouse software and equipment from multiple suppliers. Connecting these systems can prove more difficult than deploying autonomous robots themselves.
The difficulty of integrating older equipment with newer applications was one of the most important lessons from Twinsburg, although overcoming those initial obstacles made subsequent deployments considerably easier. “What took the longest was building a connector to a system that may not have something that’s publicly available like their APIs,” Surenian explains. “They needed to do some custom work to build out how to integrate with certain closed systems, but once we did that, it became easy. It was just rinse and repeat.”
The Twinsburg team developed around 30 material movement workflows, some using natural-language instructions in Copilot to generate JSON files for upload into the orchestration environment. The ability to reuse existing integrations and simplify workflow development could help manufacturers extend successful deployments across multiple production areas without repeating the same engineering work. Surenian sees further opportunities to make that process faster and more accessible.
Introducing autonomous robots into an established manufacturing operation also requires careful consideration of how employees will adapt to working alongside them. At Twinsburg, the phased deployment gave workers an opportunity to become familiar with the technology before more sophisticated autonomous processes were introduced. For Surenian, securing workforce acceptance depends on demonstrating that automation can improve the work people do rather than simply eliminate their jobs. “I think if you’re doing it to reduce workforce, it’s not going to go well,” he says. “You do need to have change management. That change management has to be that we’re doing this to try to allow our most valuable resource to become more productive.”
The next stage is decision-making
Connecting material movement to execution creates further opportunities to coordinate scheduling, maintenance and quality. A machine failure can change what needs to be produced, which materials are required and when they should arrive. Traditionally, these adjustments depend on people reconciling information across separate systems.
Production planning is particularly important because a schedule that looks efficient on paper may be impossible to execute under actual factory conditions. Material availability, equipment failures and transport constraints all influence whether orders can be completed as planned. Integrating execution feedback with planning systems could allow manufacturers to adjust schedules before small disruptions develop into significant production delays.
Surenian describes work with scheduling agents that can evaluate plans through simulation, identify constraints and recommend changes using real-time production information. The longer-term ambition is a feedback loop in which material logistics adjusts as production conditions change, rather than following a plan that may already be obsolete.
“If a piece of equipment goes down, you can update the schedule much faster than traditional methods,” he explains. “That’s where the agentic approach comes in: grabbing the feedback, translating that into actionable results that can either be directed to a human to initiate, or do it automatically via the agent.”
Giving software greater responsibility for operational decisions requires clear boundaries. AI agents changing schedules or priorities without suitable safeguards could create disruption instead of preventing it, particularly where decisions affect safety, equipment or customer commitments.
“You got to do it controlled, right? You don’t want to unleash these,” Surenian warns. “What I like about the Rockwell’s approach is it’s very pragmatic with a limited definition of what it’s supposed to do, with the appropriate control points to allow a human to intervene.”
Twinsburg shows why autonomy need not begin with a complete factory overhaul. The first step was to automate an existing transport task; the larger gains arrived when those movements became part of production execution. For manufacturers that have spent decades improving individual machines, coordinating what happens between them may be the next substantial source of productivity.
